
Rapid prototyping · Updated 2026-10-14
3D Printing Wall Thickness and Tolerance Chart (FDM, Resin, SLS/MJF).
Minimum walls, holes, clearances, overhangs and detail sizes for FDM, resin and SLS/MJF, plus FDM design rules for strong, accurate parts.
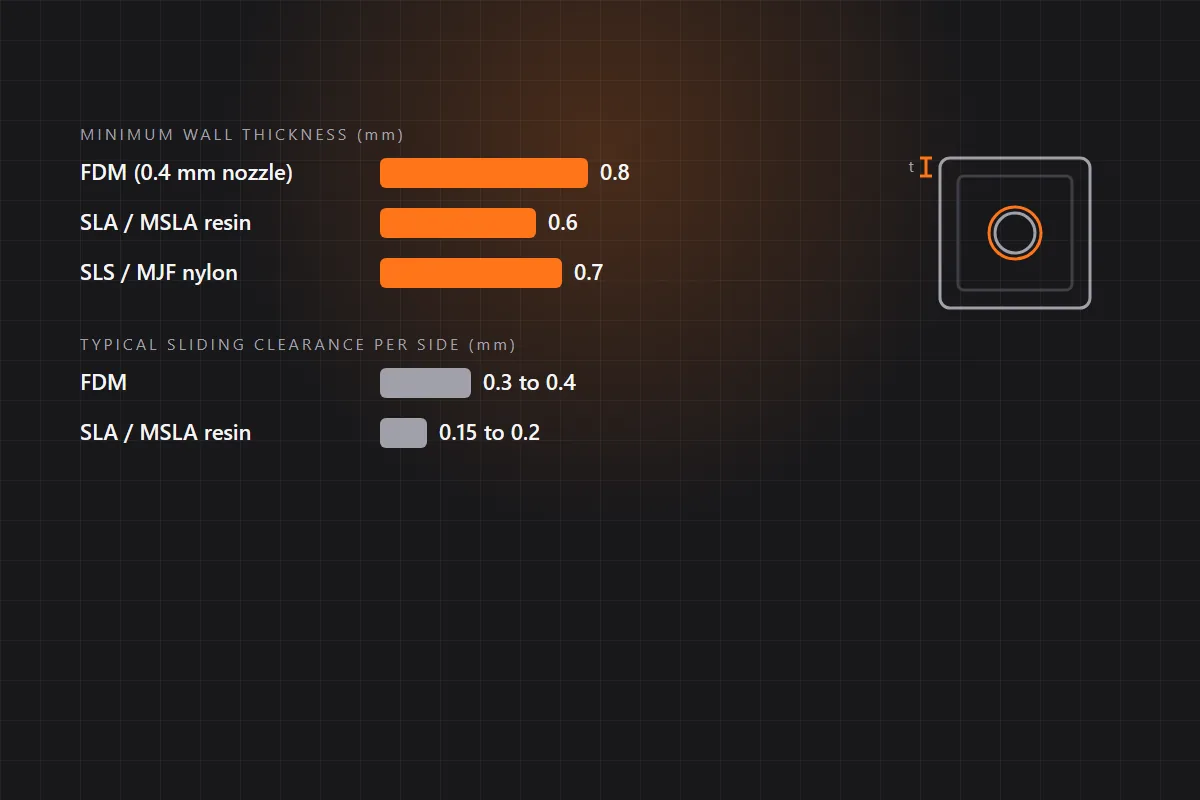
This chart gives starting values for minimum wall thickness, holes, clearances, overhangs and fine detail for FDM, resin (SLA/MSLA) and nylon powder (SLS/MJF) 3D printing. They are typical values from manufacturer design guides. Every printer and material behaves slightly differently, so print a small test piece before you commit to a tight-fitting assembly.
3D printing wall thickness and tolerance chart
| Feature | FDM (0.4 mm nozzle) | SLA / MSLA resin | SLS / MJF nylon |
|---|---|---|---|
| Minimum wall, supported (joined to other walls) | 0.8 mm | 0.6 mm | 0.7 mm |
| Minimum wall, unsupported (free-standing) | 1.0 mm | 1.0 mm | 1.0 mm |
| Recommended wall for strong parts | 1.6 to 2.4 mm | 1.5 to 2.0 mm | 1.2 to 2.0 mm |
| Minimum hole diameter | 2 mm | 0.5 mm | 1.5 mm |
| Clearance for moving parts (per side) | 0.3 to 0.4 mm | 0.15 to 0.2 mm | 0.3 to 0.5 mm |
| Embossed or engraved detail | 0.6 mm wide, 2 mm tall | 0.1 mm | 1 mm |
| Overhangs without supports | Up to 45° from vertical | Supports needed for most overhangs | Any angle |
| Unsupported bridges | Up to about 10 mm | Not recommended | Any length |
| Escape holes for hollow parts | Not needed | At least 3.5 mm | At least two holes of 5 mm |
Sources for typical values: Hubs design considerations and Hubs SLS design guide. For help choosing between processes, see FDM vs SLA vs SLS vs MJF.
Wall thickness
On FDM printers, make walls a whole multiple of the line width, which is usually the nozzle diameter. With a 0.4 mm nozzle, use 0.8 mm (two lines), 1.2 mm (three lines) or 1.6 mm and above for load-bearing parts. In-between values leave thin gaps inside the wall.
Keep wall thickness as even as possible. Thick sections next to thin ones cool at different rates and can warp FDM parts or leave sink marks on SLS and MJF parts. On powder-bed parts, hollow out sections thicker than about 4 mm and add escape holes so the powder can be removed.
Overhangs and bridges: the 45° rule
On FDM, each layer needs something underneath it. Faces tilted up to 45° from vertical print cleanly without supports. Between 45° and about 60°, they still print but the underside gets rougher. Beyond about 60°, add supports or change the design.
- Use a 45° chamfer instead of a fillet on edges that touch the build plate. A fillet starts almost flat and droops; a chamfer prints cleanly from the first layer.
- Turn horizontal holes into teardrop shapes, or accept a little roughness at the top of the hole.
- Bridges between two supports print well up to about 10 mm with good part cooling. For longer spans, add an arch or a gusset.
Resin parts almost always need supports, so orient them so support marks land on hidden faces. SLS and MJF parts need no supports at all.
Holes, fits and clearances
FDM prints small vertical holes slightly undersize, typically 0.2 to 0.4 mm smaller in diameter, because the plastic contracts as it cools. Either model the hole larger or drill it to size after printing. For an 8 mm guide rod, model the hole at 8.3 mm, or print it at 7.8 mm and ream it with an 8 mm drill.
- Sliding or rotating fit (FDM): 0.3 to 0.4 mm clearance per side.
- Sliding fit (resin): 0.15 to 0.2 mm per side.
- Bearing press fit (FDM): start with a hole 0.1 to 0.2 mm larger than the bearing's outer diameter, print a test ring, and adjust.
- Snap fits: use PETG, nylon or tough resin. PLA and standard resin tend to crack.
Strength and load direction
FDM parts are weakest where layers meet, so a part is stronger when the load runs along the printed lines rather than pulling layers apart. Orient brackets so the bending load lies in the build plane. For strength, add perimeters (wall lines) before increasing infill: four walls with 25 to 35% gyroid infill are usually stronger than two walls with 80% infill.
Avoid sharp inside corners. Add fillets of 1.5 to 3 mm to spread stress, especially where a rib meets a wall.
Screws and threads in printed parts
Printed threads wear out quickly if a screw is removed often. Better options:
- Brass heat-set inserts: size the hole to the insert maker's specification and press the insert in with a soldering iron.
- Captive nut pockets: hexagonal slots that hold a standard M3, M4 or M5 nut.
- Through-bolts: a bolt through the whole part with a washer and lock nut.
Preventing warping on large flat parts
Large flat FDM parts lift at the corners when the edges cool faster than the middle. Round the outside corners, use a brim, keep the bed at the right temperature for the material and protect the printer from drafts. ABS and ASA usually need an enclosed printer.
Frequently asked questions
What is the minimum wall thickness for 3D printing?
Typical minimums are 0.8 mm for FDM with a 0.4 mm nozzle, 0.6 mm for resin and 0.7 mm for SLS or MJF nylon. Walls that stand alone should be at least 1 mm. Use thicker walls for parts that carry load.
What tolerance should I leave between moving 3D printed parts?
Start with 0.3 to 0.4 mm per side for FDM, 0.15 to 0.2 mm for resin and 0.3 to 0.5 mm for SLS or MJF. Print a small test piece to confirm on your printer.
What is the 45-degree rule in 3D printing?
On FDM printers, surfaces tilted up to 45° from vertical can print without supports. Steeper overhangs start to sag. Beyond about 60° from vertical, add supports or redesign the feature.
Why are my printed holes too small?
FDM plastic shrinks inward as it cools, so small vertical holes usually come out 0.2 to 0.4 mm undersize. Model them larger or drill them to size after printing.
Need help with the next step?
Need a part 3D printed?
Send your CAD file and a line about what the part must do. PakMEC prints in FDM, resin, SLS, MJF and metal, and an engineer will recommend a process and quote it.